Novram
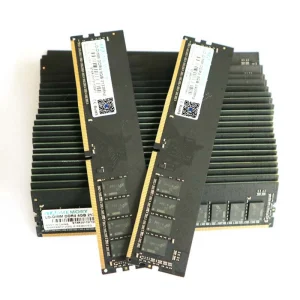
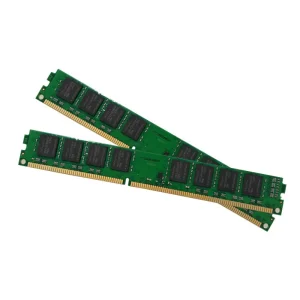
Explore our enterprise-grade electronic architecture, industrial computer motherboards, high-frequency DDR modules, and embedded PCBA assemblies configured for mission-critical vision processing.
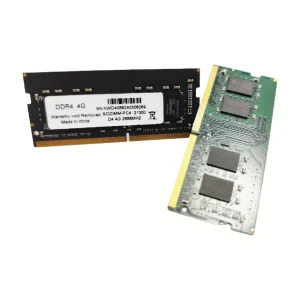
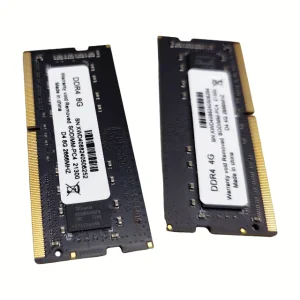
The global optics and micro-electronics market is undergoing a structural paradigm shift driven by the rapid acceleration of Edge AI, autonomous mobility, robotics, and smart surveillance infrastructure. Traditionally, optical lens manufacturing and compute hardware development existed in siloes. Today, high-resolution optical captures are tightly coupled with ultra-low latency memory subsystems, onboard ISP (Image Signal Processor) firmware, and specialized compute silicon. As a premier custom OEM camera lens manufacturer and integrated micro-electronics exporter, our engineering ethos bridges the micro-gap between optical glass physics, CMOS sensor matching, high-speed DDR memory buffering, and robust SMT PCBA assembly.
Modern machine vision applications—ranging from automated optical inspection (AOI) on industrial production lines to real-time LIDAR/ADAS sensor fusion in autonomous vehicles—demand distortion-free optical performance, extreme thermal stability, and high-frequency data pipeline throughput. Modern camera lenses are no longer passive light-gathering elements; they are precision-calibrated optoelectronic gateways designed to stream high-bitrate visual data directly into high-speed memory architectures such as DDR4/DDR5 modules and embedded compute platforms.
Key Technological Takeaway: Modern OEM camera lens engineering requires optical-to-silicon co-design. Mitigating optical aberrations (chromatic, spherical, and field curvature) at the front-end lens elements directly reduces computational overhead and thermal throttling on downstream AI vision processors and DDR memory buffers.
Optimized Modulation Transfer Function (MTF) curves ensuring crisp edge-to-edge optical resolution tailored for 4K to 8K high-density CMOS sensor pixels.
Aircraft-grade anodized aluminum and thermal-compensating optomechanical designs that maintain focal stability across extreme temperatures (-40°C to +85°C).
Seamless mechanical and electronic alignment with onboard PCBAs, high-speed RAM buffers, and heat dissipation structures for turnkey device manufacturing.
Tailored focal lengths (FL), relative apertures (F/#), optical distortion limits (<0.1%), wavelength anti-reflective coatings, and iris configurations.
Enterprise procurement managers across North America, Europe, and Asia-Pacific face complex challenges when sourcing custom optical modules and computing hardware. The global market requires camera lens manufacturers and micro-electronics exporters to deliver far more than standalone components. Today’s B2B buyers mandate full supply chain transparency, rapid NPI (New Product Introduction) cycles, strict RoHS/CE/FCC compliance, and multi-tier quality management systems.
China remains the powerhouse of global precision manufacturing, transitioning from traditional low-cost assembly to advanced Industry 4.0 automated production ecosystems. At the heart of Shenzhen’s high-tech manufacturing corridor, custom lens production and micro-electronics manufacturing benefit from unmatched supply chain cluster density. Raw glass blank pressing, optical coating, CNC metal barrel milling, Class 100 cleanroom assembly, SMT circuit surface mounting, and automated testing are co-located within a 30-minute supply chain radius.
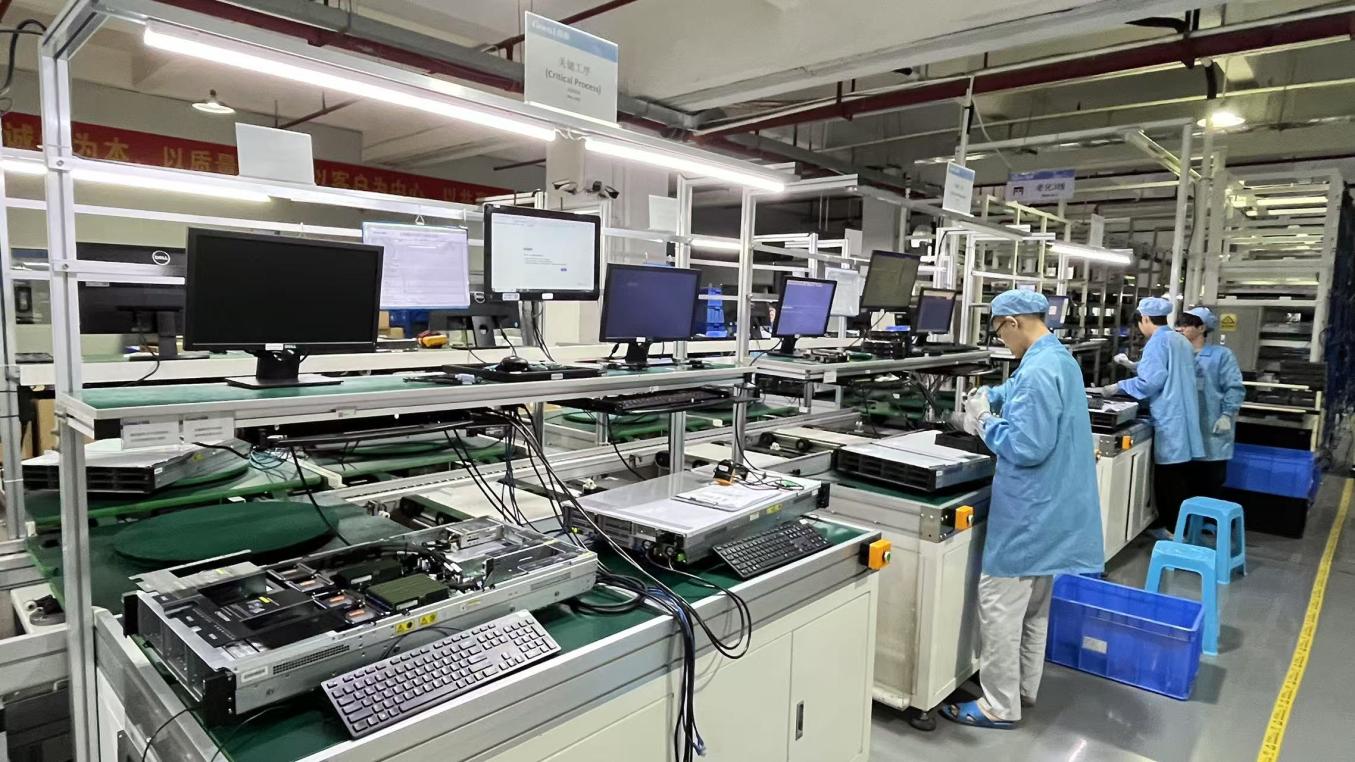
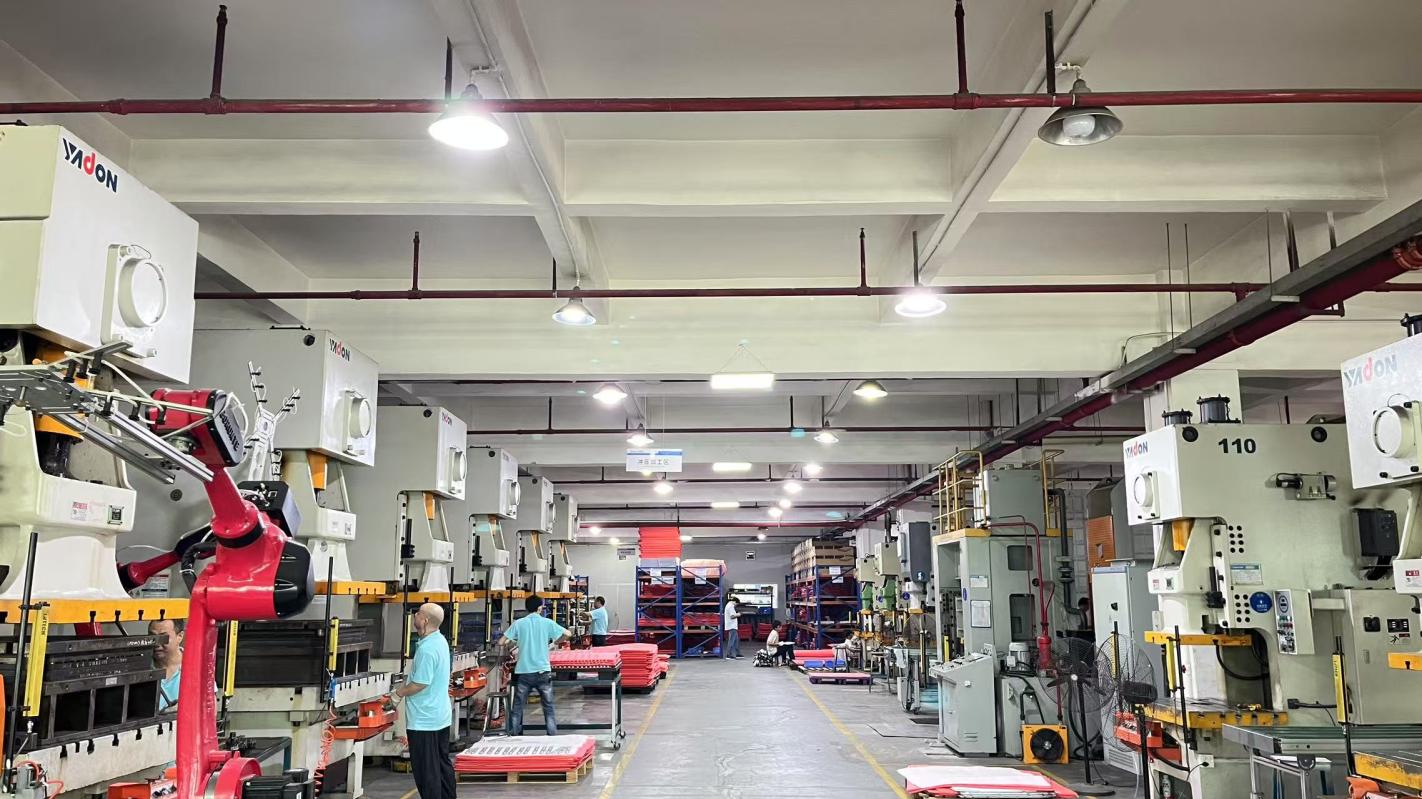
This geographic concentration of specialized vendors enables unmatched speed-to-market. Rapid optical prototyping that previously required 8 to 12 weeks in Western markets can now be executed within 10 to 14 days in Shenzhen, complete with full MTF diagnostics, thermal chamber testing, and sample hardware integration. Furthermore, highly automated robotic assembly lines significantly reduce manual human touchpoints, minimizing particulate contamination and driving yield rates above 99.4%.
Custom OEM camera lenses and integrated processing boards are deployed across an expansive array of mission-critical commercial and industrial verticals globally:
Wide-angle low-distortion lenses paired with high-frequency RAM modules enable real-time VSLAM (Visual Simultaneous Localization and Mapping) for warehouse logistics robots operating in dynamic warehouse environments.
Waterproof (IP68/IP69K), heated, anti-fog lens assemblies combined with industrial server memory components ensure reliable multi-camera capture for automated braking and lane keep assistance.
Telecentric and high-contrast fixed-focal lenses mounted on high-speed industrial motherboards inspect PCB SMT joints and semiconductor wafers at line speeds exceeding 1,000 components per minute.
Micro-aperture custom optical lenses featuring multi-layer anti-reflective coatings provide crisp, true-color video transmission into ultra-compact image processing sub-assemblies for surgical equipment.
Novram Electronics Co., Ltd. is a professional DDR5 memory manufacturer and integrated hardware engineering provider based in Shenzhen, China, dedicated to delivering high-performance DRAM solutions, PCBA processing, and optical hardware integration for global OEM, ODM, and industrial customers. Established in 2016, the company has grown into a reliable supplier of high-speed memory modules, embedded computing components, and customized hardware systems serving partners across consumer electronics, industrial automation, embedded systems, gaming, and enterprise computing.
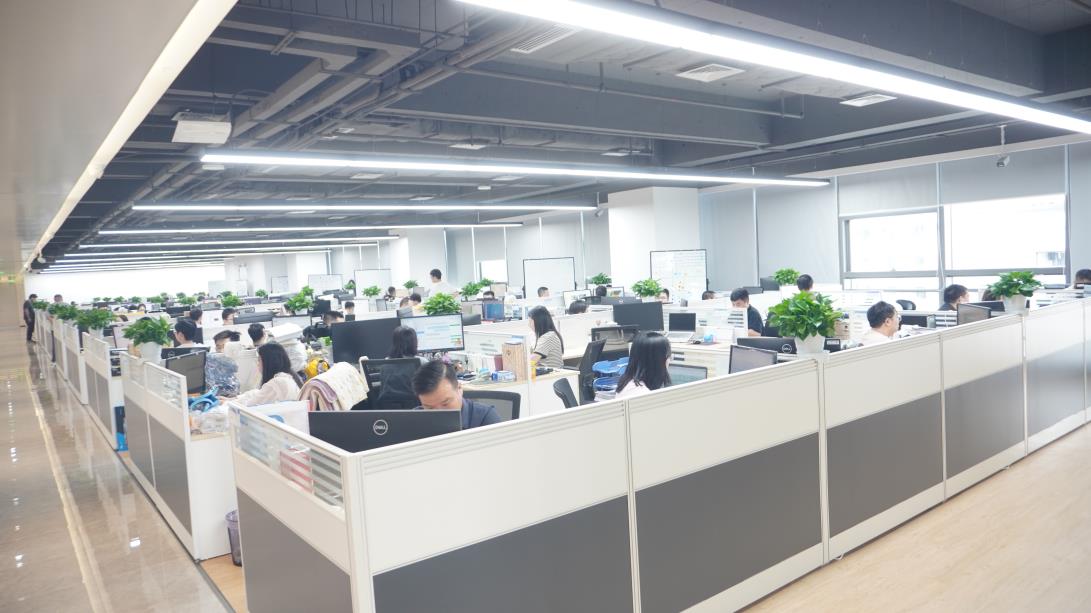
Operating from a modern 3,860㎡ manufacturing facility, Novram integrates advanced production equipment, strict quality management, and continuous R&D innovation to ensure every memory module and hardware component meets international performance and reliability standards. Our experienced engineering team focuses on developing high-speed, stable, and energy-efficient products for diverse computing and vision applications.
With 9 years of industry experience and 7 years of export experience, Novram exports products to customers in more than 40 countries. The company achieves an annual export revenue of approximately US$18.6 million, supported by an efficient global supply chain and responsive customer service.
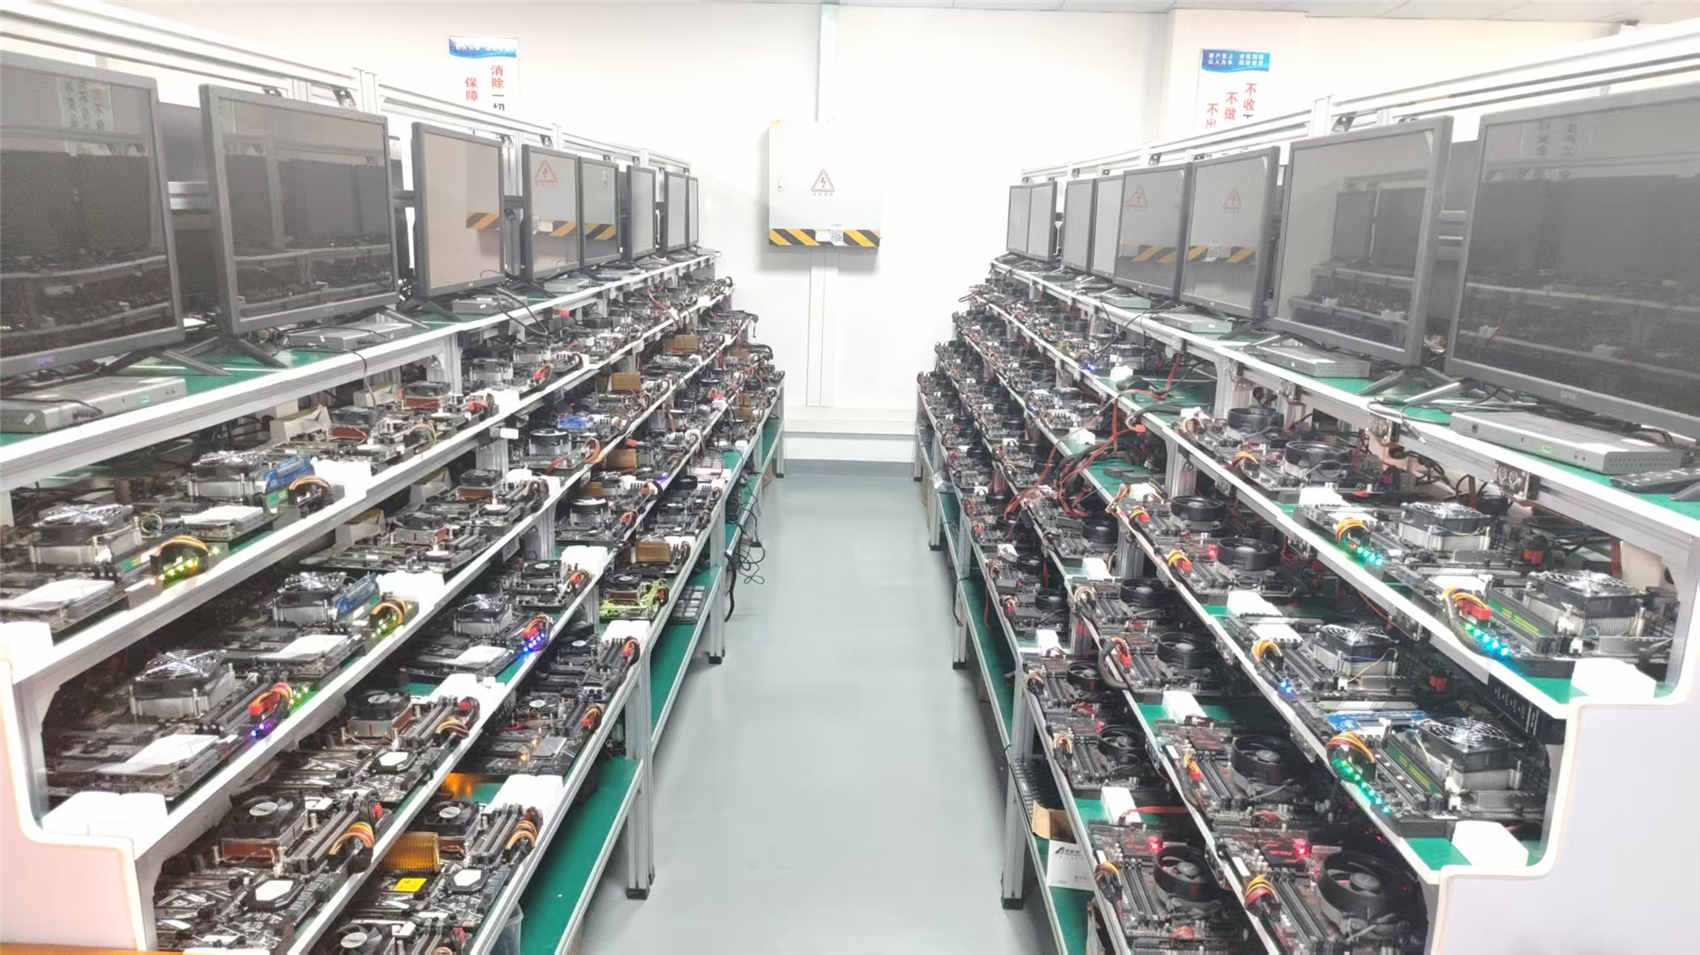
Quality is at the core of everything we do. Every product undergoes 100% functional testing, compatibility testing, burn-in testing, temperature testing, and aging verification before shipment. Our quality control department consists of 42 professional inspectors, ensuring consistent product performance and long-term reliability.
Novram maintains strong partnerships with over 860 qualified supply chain partners, enabling stable production capacity and reliable component sourcing. Our primary customers include memory module brands, computer manufacturers, industrial PC companies, system integrators, distributors, wholesalers, and OEM/ODM partners worldwide.
Innovation drives our competitiveness. Our dedicated R&D center is staffed by 76 experienced engineers, allowing us to introduce approximately 138 new products each year. We provide comprehensive OEM, ODM, private label, logo printing, packaging customization, capacity customization, firmware optimization, and product specification customization to meet different market requirements.
Today, Novram continues to invest in advanced manufacturing technologies, strict quality assurance, and customer-focused innovation. Our mission is to become a trusted global partner for high-performance compute and vision memory solutions by delivering reliable products, flexible customization, competitive pricing, and professional technical support.
Technical specifications, customization workflows, minimum order quantities, and global exporter logistics.
Explore our complete catalog of industrial computer components, memory sticks, thermal dissipation hardware, and custom PCBA solutions engineered for long-term operational stability.